
How to Choose a Reliable Automotive Electronics Manufacturer in China: A Buyer’s Checklist
Oct 19,2026
Choosing the wrong automotive electronics manufacturer can be very costly. A defect in ordinary consumer electronics may cause returns. A defect in automotive electronics can create vehicle compatibility problems, electromagnetic interference, software faults, batch claims and brand liability. At Parwatt I see buyers face these risks when supplier selection rests only on price and a polished sample.
Selecting a reliable automotive electronics manufacturer in China requires verification of legal identity, certification scope, engineering capability, production controls, traceability and change management. In 2026 buyers who follow a structured approval process reduce quality escapes and protect long-term supply.
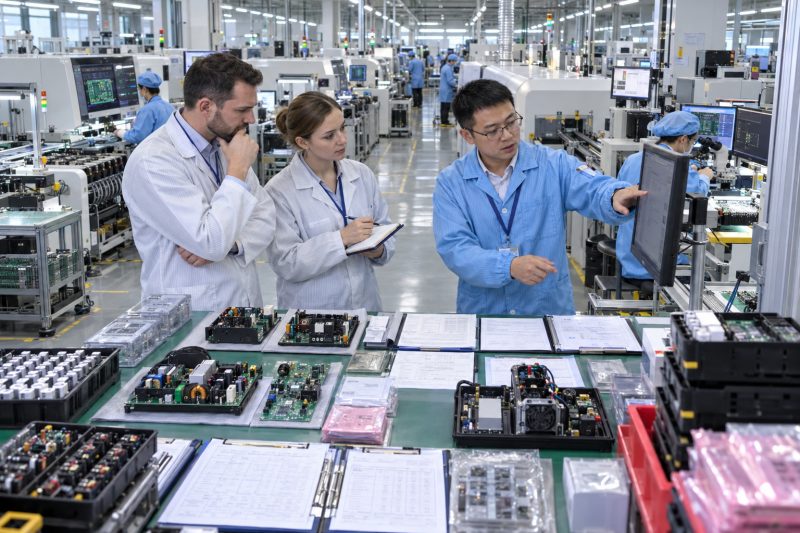
I have worked with automotive accessory brands, importers and distributors for years as general manager at Parwatt New Energy. We manufacture and supply products such as car battery chargers, tire inflators and related electronics. I regularly review supplier decisions where certificates were accepted at face value or where a perfect hand sample later failed in vehicle conditions. Our own processes for products in categories such as the car battery charger category and the car air pump category follow structured engineering and quality controls. In this article I explain how B2B buyers can choose a reliable automotive electronics manufacturer in China in 2026.
Why Choosing the Wrong Automotive Electronics Manufacturer Can Be So Costly?
Automotive electronics operate in a demanding environment. Voltage swings, temperature extremes, vibration, electromagnetic noise and long service life all apply. When a manufacturer lacks proper design control, component management or production testing, defects may pass a simple bench check and still fail in the vehicle. The commercial damage then extends beyond ordinary returns.
Choosing the wrong manufacturer is costly because automotive electronics failures can cause vehicle compatibility issues, EMC problems, software faults, batch recalls and brand liability—not only simple product returns.
How Supplier Weakness Turns into Large Losses
I have seen programs delayed for months because a supplier could not stabilise firmware after vehicles reported intermittent faults. The original sample had worked on a laboratory bench. Real vehicle power and communication conditions exposed gaps in validation.
EMC problems create another expensive class of failure. A product that ignores vehicle-level electromagnetic requirements can disturb radios, sensors or control modules. Diagnosis is time-consuming and the commercial impact spreads to the vehicle owner and the brand.
Component substitutions without approval are a frequent root cause. A capacitor, power device or wireless module is changed for cost or availability. The change is invisible on the invoice yet alters thermal behaviour, emissions or longevity. Claims appear months later and are hard to contain without batch traceability.
Software and parameter control add further risk. Unversioned firmware or uncontrolled calibration data make it impossible to know which units in the field contain which logic. Corrective action then becomes broad and costly.
Here is a table that links supplier weakness to commercial damage:
| Supplier Weakness | Typical Field Result | Commercial Impact |
|---|---|---|
| Weak vehicle validation | Intermittent faults in real cars | High support and claim cost |
| Poor EMC control | Interference with vehicle systems | Brand and liability exposure |
| Unapproved part changes | Late reliability failures | Batch risk and rework |
| No firmware version control | Unpredictable behaviour | Difficult field containment |
| Weak traceability | Cannot isolate bad lots | Broad recalls or replacements |
This table reflects the costly patterns I discuss with buyers. At Parwatt we treat automotive electronics programs with stricter controls than ordinary consumer accessories, including products related to our car vacuum cleaner category when electronic control is involved.
In 2026 vehicle systems are more sensitive and connected. The cost of a weak manufacturer continues to rise.
The Supplier Certificates and Sample Results Buyers Often Misread
Certificates and perfect samples create false confidence when they are not verified. Buyers sometimes accept scanned certificates, factory photos and one good sample without confirming the legal company, manufacturing address, certification scope and validity, or without establishing whether the supplier is the real manufacturer or a trading company.
Certificates and sample results are often misread when buyers skip verification of company identity, address, scope and validity, and when hand-built samples are treated as proof of production capability.
Verification Steps That Prevent False Confidence
An IATF 16949 or similar automotive certificate should be checked against the exact legal entity and manufacturing site. The scope must cover the relevant activities. An expired or mismatched certificate does not support the project.
ISO 9001 is useful but is not a substitute for automotive-specific process discipline. Buyers should understand what each certificate actually covers.
Factory photos and video tours show appearance, not process control. A clean workshop does not prove calibrated test equipment, controlled BOM usage or effective nonconforming-material handling.
A perfect engineering sample may be hand-built with selected parts and extra attention. It does not prove that the mass-production line, operators and ordinary material lots can repeat the same result.
Trading companies can be legitimate partners, yet the buyer must know where design control, production and testing actually occur. Responsibility becomes unclear when the named supplier cannot change the process or the BOM.
Here is a table of documents and results that need deeper checking:
| Item Presented | Common Misreading | What to Verify |
|---|---|---|
| Certificate scan | Assumed valid and relevant | Entity, site, scope, validity, issuer |
| Factory photos | Assumed controlled production | Process audits and records |
| Perfect sample | Assumed production-ready | Pilot from intended line |
| Supplier claims “manufacturer” | May be trading role | Business license, process ownership |
| Generic test report | Assumed product-specific | Model, hardware, firmware coverage |
This table keeps document review rigorous. At Parwatt we expect partners to verify the same points when assessing any electronics supplier, including those connected with our main site.
I advise buyers to treat every certificate as a starting point for verification, not as a final answer. The same discipline applies to samples.
What to Audit in Engineering, Production and Quality Control
A meaningful audit covers engineering capability, production processes and quality systems. Buyers should examine hardware and firmware development, BOM and approved-vendor control, SMT and assembly processes, AOI/ICT/FCT testing, calibration, environmental and EMC validation, traceability and nonconforming-product control.
Audit engineering, production and quality control for design competence, BOM discipline, manufacturing process control, functional and environmental testing, calibration, traceability and nonconforming-material handling.
Key Audit Areas
Engineering review should confirm that the supplier can translate requirements into schematics, PCB layouts, firmware architecture and design-failure-mode analysis. Version control for hardware and software must be visible.
BOM management must link each production batch to approved component manufacturers and part numbers. Alternative parts need formal evaluation, not informal substitution.
Production audit should cover SMT process control, conformal coating or potting where required, torque and assembly standards, and in-process inspection points.
Test coverage must include optical or automated inspection, in-circuit testing where applicable, and functional testing that exercises the real operating modes of the product. End-of-line tests should be recorded against serial or batch identity.
Calibration status of key instruments must be current. Uncalibrated fixtures produce numbers that cannot be trusted.
Environmental and EMC evidence should match the product’s intended vehicle installation and destination markets. Generic reports for a different construction are insufficient.
Quality-system audit should confirm quarantine of nonconforming material, root-cause analysis methods, corrective-action tracking and retention of quality records.
Here is an audit focus list:
- Hardware and firmware design capability
- Design review and version control records
- Approved vendor list and BOM control
- SMT, assembly and in-process controls
- AOI / ICT / FCT and end-of-line test coverage
- Instrument calibration status
- Environmental and EMC validation evidence
- Batch and serial traceability
- Nonconforming product handling
- Corrective-action and change records
At Parwatt we maintain these controls across our electronics manufacturing for products such as those in the car battery charger category.
I recommend that buyers use a written audit checklist and score each area. Subjective impressions alone are not enough for automotive electronics.
What Separates an Automotive-Grade Partner from a Consumer Electronics Factory
An automotive-grade partner operates with stricter design review, version control, engineering change management, failure analysis, batch traceability, vehicle-level validation and long-term product support. A consumer electronics factory may produce attractive samples and competitive prices yet lack the discipline required for vehicle applications.
An automotive-grade partner differs from a consumer electronics factory through rigorous design control, formal change management, structured failure analysis, full traceability, vehicle validation and sustained lifecycle support.
Practical Distinguishing Marks
Design reviews in an automotive-oriented organisation include requirements tracing, worst-case analysis and design-for-manufacturing checks. Changes after approval follow a formal process with impact assessment.
Engineering change management records who requested a change, why it was needed, what was affected and who approved it. Silent substitutions are treated as a process failure.
Failure analysis capability includes the ability to analyse returned units, identify root cause, and implement corrective actions that are verified on subsequent production. “Replace and ship” is not accepted as a complete response.
Traceability links finished units to component lots, firmware versions, assembly lines and test results. Without this link, field problems cannot be contained efficiently.
Vehicle validation goes beyond bench functional tests. Depending on the product, it may include supply-voltage variation, transients, temperature cycling, vibration, EMC and installation-level checks.
Lifecycle support covers spare parts, firmware maintenance, documentation updates and notice periods before discontinuation. Automotive programs often outlast typical consumer product cycles.
Here is a comparison of the two profiles:
| Capability | Consumer Electronics Factory | Automotive-Grade Partner |
|---|---|---|
| Design control | Basic functional focus | Formal reviews and documentation |
| Change management | Informal / flexible | Written approval and impact review |
| Failure analysis | Limited | Structured root-cause and CAPA |
| Traceability | Often batch-only or weak | Component-to-unit linkage |
| Validation | Bench and basic safety | Vehicle and environmental focus |
| Lifecycle support | Short | Planned long-term support |
This comparison helps buyers recognise the difference in practice. At Parwatt we operate automotive-oriented controls for electronics that must perform reliably in vehicle environments.
I advise buyers to ask for examples of past change-control records and failure-analysis reports. The quality of those documents reveals the real operating culture.
A Step-by-Step Supplier Approval Process Before Mass Production
A reliable approval process moves from clear requirements to verified production capability. Buyers should define technical and market requirements, verify company and certificate identity, audit the factory, test engineering samples, run pilot production, approve a golden sample, validate the mass-production line and then monitor ongoing delivery and quality.
Approve a supplier through defined requirements, certificate and identity checks, factory audit, engineering-sample tests, pilot production, golden-sample sign-off, mass-production line validation and continuous performance monitoring.
Approval Sequence
Write a complete specification covering electrical limits, mechanical interface, firmware behaviour, environmental conditions, EMC expectations, target markets and compliance documents.
Verify the supplier’s legal entity, manufacturing address and the scope and validity of relevant certificates.
Conduct an on-site or structured remote audit of engineering, production and quality systems using the checklist described earlier.
Test engineering samples against the full specification, including vehicle-relevant conditions where possible. Record results against acceptance criteria.
Authorise a pilot build on the intended production line with planned materials, tooling, operators and tests. Review first-pass yield, failures, calibration records and traceability data.
Approve a golden sample that includes the final hardware, firmware version, labels and packaging. Freeze the BOM and critical process parameters.
Confirm that mass-production inspection plans, test coverage and packaging methods match the pilot.
Release volume orders only after the above gates are closed. Maintain ongoing monitoring of incoming quality, field claims and delivery performance.
Require written notification and re-approval before any change to critical components, PCB, firmware, factory or test methods.
Here is an approval process checklist:
- Complete technical and market specification issued
- Legal entity and certificate verification completed
- Engineering, production and quality audit scored
- Engineering samples tested to specification
- Pilot run executed on intended line
- Golden sample signed and BOM frozen
- Mass-production test and inspection plan confirmed
- Change-notification agreement in place
- Ongoing quality and delivery metrics defined
- Escalation path for deviations agreed
At Parwatt we follow a comparable gated process for our own electronics programs and expect the same discipline from partners. Buyers can apply this sequence to any automotive electronics category, including products associated with our car air pump category and broader offerings on our main site.
A completed approval file does not eliminate all risk, yet it dramatically reduces the chance that basic capability gaps reach mass production. That reduction is the practical goal of the checklist.
Conclusion
Choosing a reliable automotive electronics manufacturer in China requires more than comparing quotations, certificates, and showroom samples. At Parwatt we apply structured engineering and quality controls so partners receive stable production and transparent problem-solving. Buyers should first define the product’s electrical, mechanical, software, environmental, and market-compliance requirements. They should then verify the manufacturer’s legal identity, certification scope, engineering resources, component controls, production tests, traceability system, and change-management process. Samples must be tested under realistic vehicle conditions, while pilot units should be produced on the intended mass-production line. A signed golden sample, controlled BOM, approved firmware version, inspection plan, and written change-notification agreement help protect repeat-order consistency. The strongest supplier is not necessarily the lowest bidder—it is the partner that can demonstrate stable production, transparent problem-solving, and reliable lifecycle support.
--- END ---
Related Posts


Business Ideas

Business Ideas
